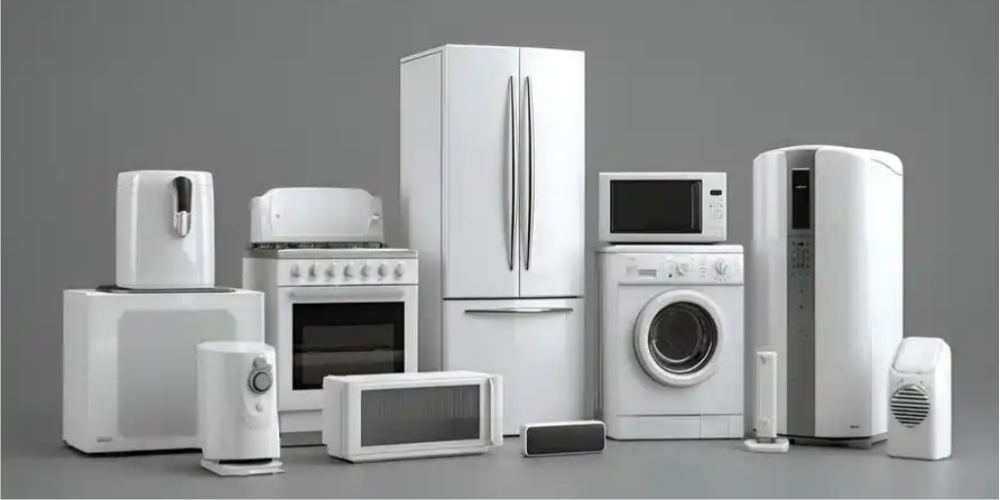
Critical Process Guidelines for Rigid Polyurethane Foam Pouring in Household Appliance Insulation
1. Raw Material Handling and Shelf-Life Management
Sealing & Moisture Control – Both the blend polyol (white component) and polymeric MDI (black component) are hygroscopic. Ingress of moisture causes undesirable side reactions (urea formation) and blowing agent loss. Containers must be resealed immediately after each use.
Storage Conditions – Store in a dry, shaded, well-ventilated area at 15–20 °C. Periodic degassing of drums is required to relieve internal pressure from dissolved inert gases.
Pot-Life Indication – A noticeable increase in viscosity of either component signals approaching the end of usable shelf life; such material shall be discarded.
2. Thermal Management – The Most Influential Variable
All temperature zones must be stabilised before production:
|
Parameter |
Recommended Range |
Effect of Deviation |
|
Ambient |
20–30 °C |
Too high → runaway reaction; too low → extended demould time |
|
Raw material (both components) |
20–30 °C (preferably matched) |
Mismatch causes inconsistent nucleation and cell structure |
|
Mould surface |
40–50 °C |
Low mould T → higher density, thick skin; high T → lower density, risk of shrinkage |
Maintain mould temperature uniformity (±2 °C) to avoid local density gradients.
3. Reaction Kinetics and Process Window
For machine dispensing (high-pressure impingement mixing), The cavity must be completely filled before the gel point (string time). Otherwise, flow stops prematurely, leading to voids and poor adhesion to liners.
4. Pouring Strategy and Filling Optimisation
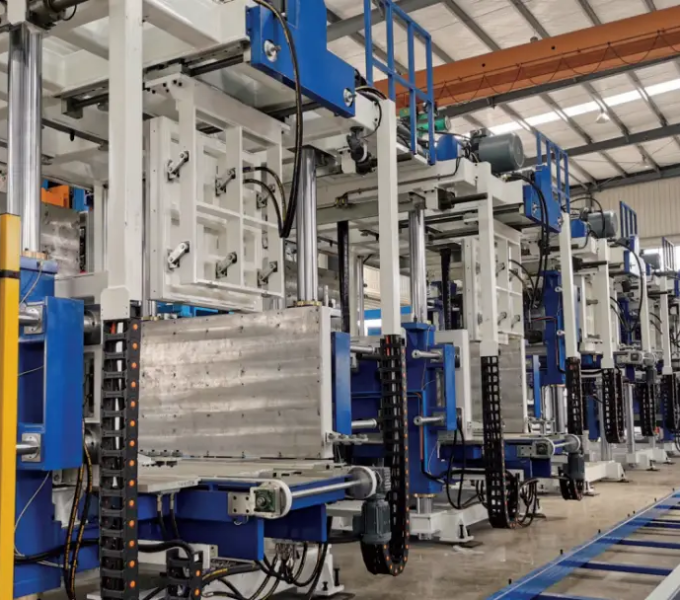
Injection port positioning – Place ports near the geometric centre of the largest unfilled volume, considering gravity flow and obstacles (evaporator tubes, internal structures).
Overpack ratio – Operate at 10–15 % overpack relative to theoretical cavity volume. This compensates for post-demould shrinkage and reduces anisotropy between vertical and horizontal cell orientation. Avoid excessive overpacking (>18 %) in closed moulds to prevent shell deformation.
Catalyst selection – Use delayed-action amine catalysts to extend cream time for better flow without sacrificing demould performance.
6. Post-Curing and Demoulding Discipline
Premature demoulding causes post-expansion distortion and weakened adhesive bond between foam and liners. After demoulding, parts must undergo a post-cure phase at elevated temperature (≥ 50 °C) for a sufficient duration (typically 2–4 h) to complete the crosslinking reaction and stabilise dimensions.
7. Typical Defects – Root Cause Analysis
|
Defect |
Most Likely Causes |
|
Surface friability |
Under cure (insufficient index or too short demould time) |
|
Excessive shrinkage |
Incorrect ratio (low index), poor mixing, or over fast gelation |
|
Voids / air traps |
Improper venting, low mould temperature, or inadequate injection pressure |
|
Density stratification |
Mould temperature gradient or non uniform overpack distribution |
|
Poor adhesion to liner |
Contaminated substrate surface or too low mould temperature at contact area |
8. Occupational Health and Process Safety
Personal protective equipment (PPE) – Impervious gloves (nitrile), chemical resistant apron, and full face shield. Replace gloves frequently.
Ventilation – Local exhaust ventilation must be operational; airborne isocyanate concentrations must be kept below the occupational exposure limit (e.g., 0.005 ppm as NCO).
Emergency protocol – Skin contact: wash thoroughly with soap and water. Eye contact: irrigate with water for at least 15 minutes and seek immediate medical attention.
Mould safety – Never close a mould without functional vent holes – rapid exothermic reaction can generate dangerous internal pressure, risking mould rupture.
Hot work prohibition – No welding, grinding, or open flame operations near uncured foam (blowing agents are flammable).